Economizer Coils Manufacturer India | IBR Boiler Economizers
Bare & Finned Waste Heat Recovery Blocks to Boost Thermal Efficiency
Modern Boilers bare tube and spiral high-frequency welded finned economizers recover sensible heat from escaping boiler flue gases to preheat incoming boiler feedwater. Each 6°C rise in feedwater temperature increases boiler efficiency by 1%, yielding immediate fuel cost savings across continuous industrial operations.
What is Economizer Coils?
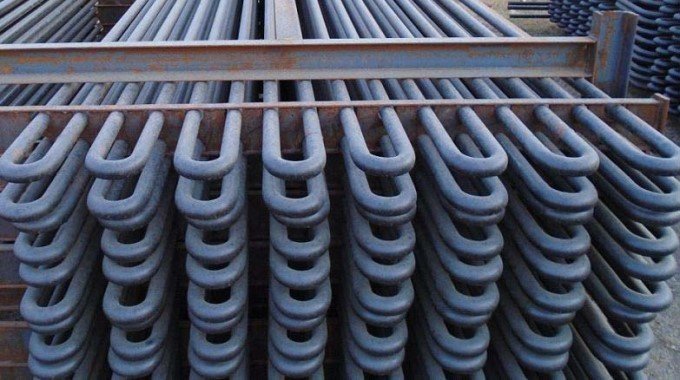
Economizer Coils are tubular heat exchanger bundles installed in boiler flue gas ducts that recover sensible waste heat to preheat incoming feedwater before entering the boiler drum. Modern Boilers Pvt. Ltd. manufactures plain bare tube, rectangular H-finned, and high-frequency spiral finned Economizer Coils under Indian Boiler Regulations (IBR 1950 Regulation 338-342). Every 6°C feedwater temperature rise achieved across our economizer blocks increases boiler thermal efficiency by approximately 1% (4% to 8% overall fuel savings), tested with pneumatic submerged bubble testing and hydro-pressure up to 200 kg/cm².
Manufacturing & Engineering Parameters
Every component is designed, formed, and tested under strict adherence to the Indian Boiler Regulations 1950 and ASME Section I Power Boilers code.
| Tube Metallurgy | BS 3059 Part 2, ASTM SA210 Gr. A1 / Gr. C, SA106-B |
| Fin Type | Plain bare tube, H-finned, and Spiral serrated finned |
| Tube Outer Diameter | 31.8 mm, 38.1 mm, 44.5 mm |
| Wall Thickness | 3.2 mm to 4.5 mm |
| Inlet Water Temp | 105°C (Deaerator outlet) |
| Outlet Water Temp | 180°C to 240°C preheated feedwater |
| Thermal Efficiency Gain | 4% to 8% overall boiler fuel efficiency increase |
| Header Connections | Full penetration socket or butt weld into collector headers |
| Hydrostatic Test | Tested up to 200 kg/cm² |
Industrial Applications & Boiler Types
- Process boilers in chemical, fertilizer, and textile manufacturing plants
- Thermal power stations seeking flue gas temperature reduction below 140°C
- Biomass and stoker fired boilers with high flue gas heat availability
- Retrofit economizer blocks for older, low-efficiency boilers
Quality Control & NDT Testing
- Precision continuous serpentine coils with automated spacer support assemblies
- Pneumatic submerged leak testing in illuminated water immersion testing tank
- Fin-to-tube bonding strength tested by destructive strip peel protocols
- Certified IBR Form III-A documentation delivered with every unit
Direct heavy trailer dispatch from Nagpur MIDC to Chandrapur (3 hrs), Bhilai (6 hrs), Raipur (7 hrs), and Hazira (20 hrs).
Frequently Asked Engineering & Procurement Questions
Technical answers curated directly by our senior boiler design engineers for plant heads, O&M managers, and procurement teams.
Request Technical Quote & Drawing Review
Submit your tube schedule, drawing number, or replacement bill of quantities (BOQ). Our engineering desk in Nagpur provides commercial proposals within 4 business hours.
Related Boiler Pressure Parts & Fittings
Modern Boilers designs and manufactures high-performance radiant, platen, and convective superheater coils for high-pressure power generation and industrial process boilers. Cold mandrel bent with strict ovality limits and post-weld heat treatment, our coils ensure maximum steam enthalpy and heat absorption while resisting high-temperature flue gas corrosion and creep fatigue.
Generating bank tubes connect the upper steam drum to the lower mud drum in bi-drum water-tube boilers. Precision bent on computerized mandrel benders, each tube is guaranteed to exact curvature templates. Specially annealed tube ends ensure zero-leak roller expansion tightness into drum tube holes without work-hardening or micro-cracking.
Modern Boilers feedwater storage tanks and deaerator columns prevent boiler tube pitting and dissolved oxygen corrosion. By elevating water temperature to 105°C and stripping non-condensable gases below 0.005 cc/liter, our vessels ensure reliable suction head for high-pressure feedwater pumps and buffer boiler surge loads.